A Practical Troubleshooting and Fiber Quality Control Guide for Spinning Mills and International B2B Buyers
Consistent fiber quality is essential for efficient polyester yarn spinning. Even when two polyester staple fiber grades have the same nominal denier and cut length, they may behave differently during opening, carding, drawing, and spinning.
For spinning mills using virgin or recycled polyester staple fiber products, unexpected variation in raw material characteristics can contribute to yarn unevenness, end breakage, excessive waste, processing interruptions, and inconsistent finished yarn quality.
However, not every yarn defect is caused by the fiber itself. Machine settings, equipment condition, blending practices, environmental conditions, and operating procedures can produce similar symptoms.
Understanding common fiber quality issues in polyester yarn spinning helps manufacturers investigate problems systematically rather than replacing raw materials without identifying the actual cause.
This guide examines ten important fiber-related quality issues, explains how they may affect spinning performance, and provides practical recommendations for technical teams and international procurement managers.
1. Why Fiber Quality Matters in Polyester Yarn Spinning
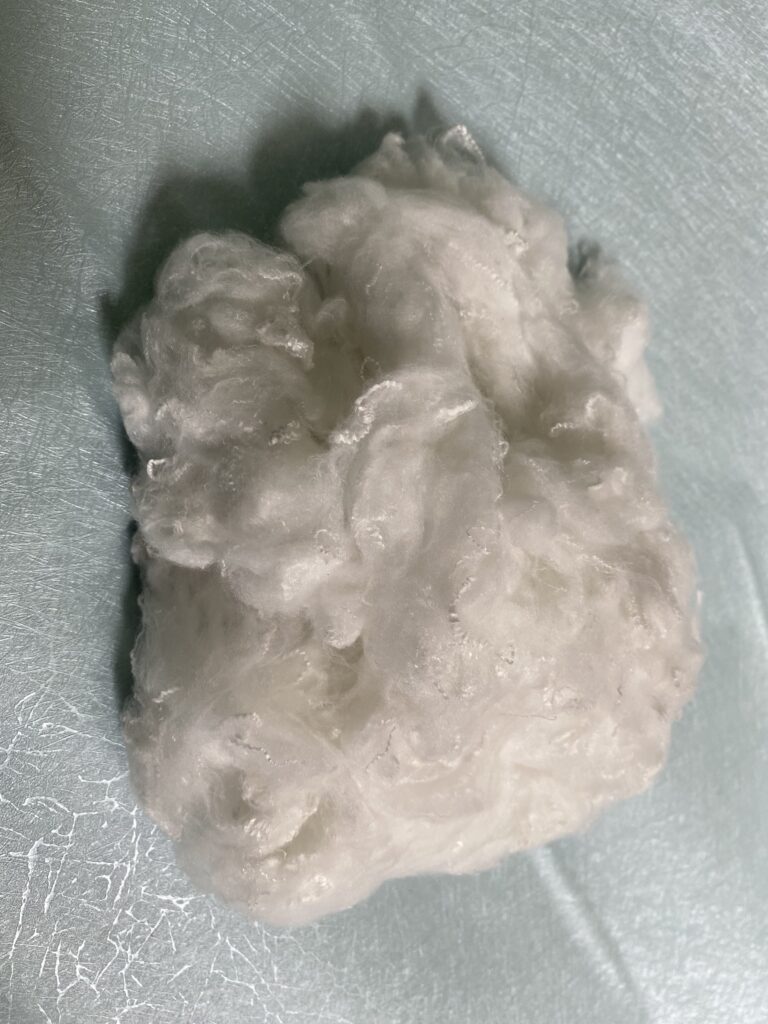
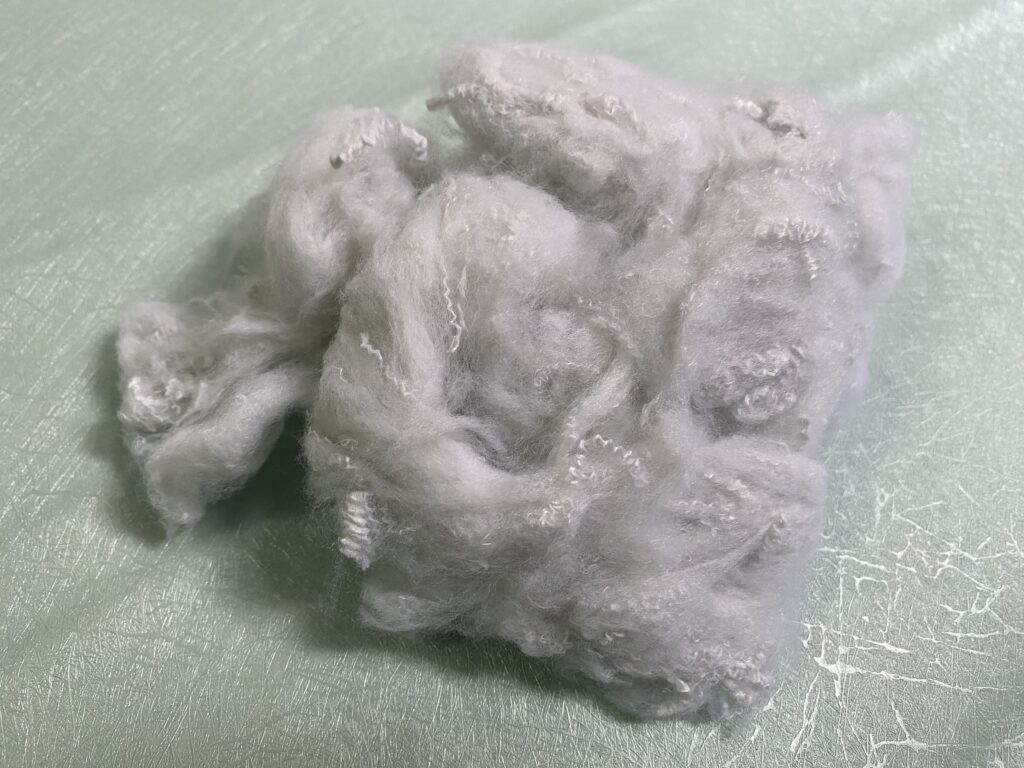
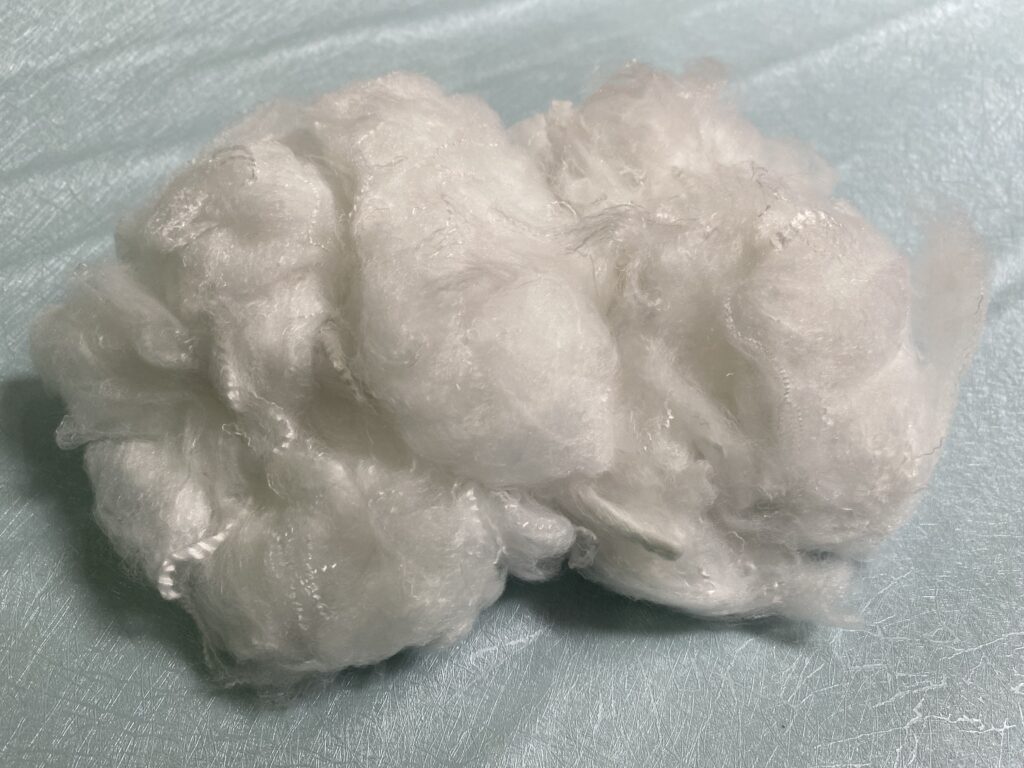
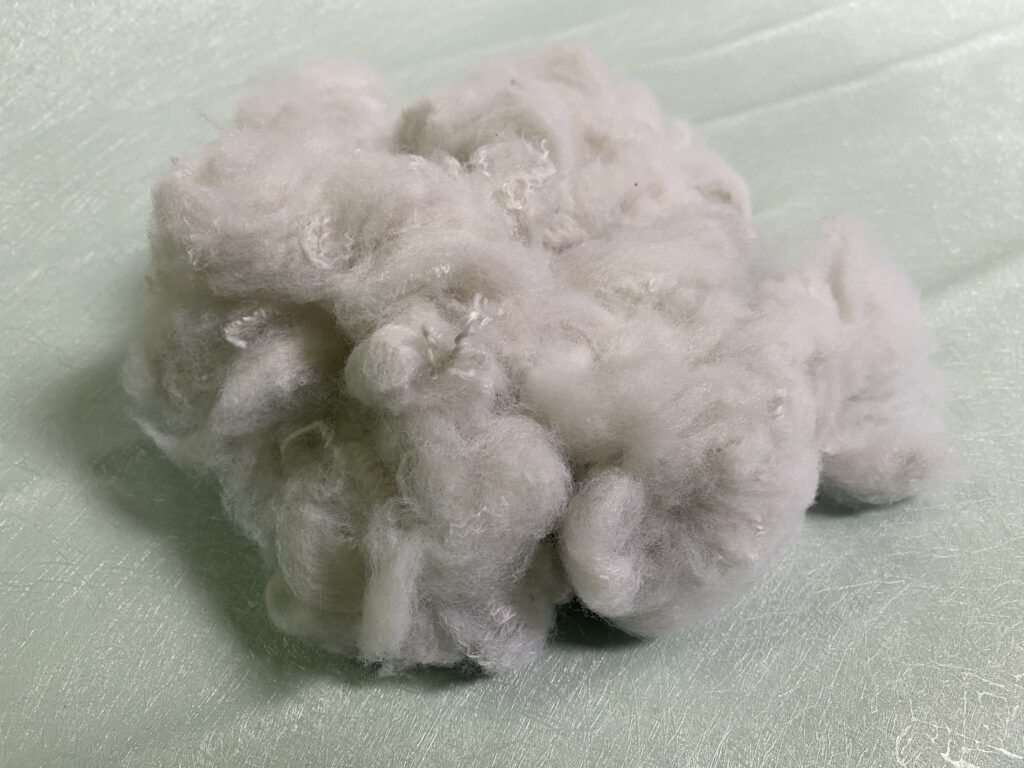
Recycled polyester fiber for yarn spinning either as a primary raw material or in blends with cotton, viscose, and other compatible fibers.
The spinning process generally involves several stages, depending on the production system:
- Fiber opening and preparation
- Blending, where required
- Carding
- Drawing
- Roving, where applicable
- Yarn spinning
- Winding and yarn inspection
Different systems, such as ring, rotor, and air-jet or vortex spinning, have different fiber requirements and processing conditions.
The quality of the incoming fiber can influence:
- Fiber opening and separation
- Carding stability
- Sliver uniformity
- Drafting behavior
- Yarn evenness
- End-break frequency
- Yarn strength and elongation
- Hairiness
- Waste generation
- Finished fabric appearance
A stable fiber supply supports more predictable production, but raw material consistency must be evaluated together with the mill’s equipment and process controls.
2. Inconsistent Fiber Denier
Denier describes the linear density of a fiber.
It is an important specification when selecting polyester staple fiber for a particular yarn count and spinning system.
Possible Problems
Variation in fiber fineness may contribute to:
- Uneven fiber distribution in the yarn cross-section
- Changes in drafting behavior
- Inconsistent yarn appearance
- Variation in yarn mechanical properties
- Differences in processing behavior between production lots
These effects depend on the magnitude of the variation and the spinning process.
How to Investigate
A spinning mill can compare fiber fineness measurements from the affected lot against its approved material specification.
The technical team should also review yarn count, drafting conditions, and other process variables.
What Buyers Should Ask Suppliers
Request the nominal denier, applicable tolerance, test method, and available inspection results.
The supplier should confirm which measurements are included in its routine quality control.
3. Cut-Length Variation and Excessive Short Fibers
Staple length is another critical factor in spinning.
Polyester staple fiber is manufactured to a nominal cut length, but the actual length distribution may contain variation.
Possible Problems
An unsuitable length distribution or excessive short-fiber content may contribute to:
- Reduced fiber control during drafting
- Higher waste generation
- Yarn unevenness
- Increased hairiness
- More frequent end breaks
- Processing difficulties in certain spinning systems
The relationship between fiber length and spinning performance depends on the equipment and target yarn.
How to Investigate
Review the incoming fiber length distribution and compare it with the approved specification.
Check whether the problem occurs across multiple machines or is concentrated in particular positions.
If short-fiber content appears to increase during processing, inspect the opening and carding stages for possible fiber damage.
Procurement Recommendation
Ask for more than a nominal cut-length label when length consistency is critical.
Where necessary, agree on an appropriate measurement method and acceptance criteria.
4. Excessive Fiber Contamination
Contamination is an important concern in both recycled and virgin polyester fiber processing.
Potential contaminants may include:
- Foreign fibers
- Colored fiber fragments
- Plastic fragments
- Dust
- Packaging material
- Other unwanted particles
The type and severity of contamination depend on the raw material and manufacturing process.
Possible Problems
Contamination can contribute to:
- Visible yarn defects
- Unexpected color variation
- Equipment cleaning requirements
- Yarn quality rejection
- Additional processing waste
- Customer complaints about finished fabric appearance
Foreign material can be particularly problematic in applications with strict appearance requirements.
How to Investigate
Inspect samples from unopened bales and compare them with material collected during opening and carding.
This helps distinguish contamination already present in the raw fiber from contamination introduced during handling or processing.
Where possible, record the type, frequency, and source of foreign material.
Procurement Recommendation
Define cleanliness requirements clearly.
Avoid relying on vague descriptions such as “100% clean fiber” without an agreed inspection method or acceptance criterion.
5. Inconsistent Fiber Crimp
Crimp refers to the waviness of staple fibers.
Crimp characteristics can influence fiber cohesion, opening, carding, and drafting behavior.
Possible Problems
Inconsistent crimp may be associated with:
- Irregular fiber opening
- Variation in web or sliver formation
- Changes in fiber cohesion
- Drafting instability
- Differences in processing behavior between lots
Both insufficient and excessive crimp may create difficulties under certain processing conditions.
How to Investigate
Compare crimp characteristics between approved and problematic fiber lots.
Review opening, carding, and drafting settings to determine whether the material is being processed appropriately.
Procurement Recommendation
When crimp is important for the intended spinning system, agree on the relevant characteristics and measurement procedure rather than requesting a generic “high-crimp” or “low-crimp” product.
6. Low or Inconsistent Fiber Tensile Strength
Fiber tensile properties are relevant to processing and finished yarn performance.
However, individual fiber strength should not be confused with finished yarn strength.
Yarn strength also depends on fiber arrangement, twist, drafting, yarn structure, and other variables.
Possible Problems
Fiber strength variation may contribute to:
- Increased fiber breakage during processing
- Changes in yarn tensile performance
- Higher short-fiber generation
- Inconsistent production results
These symptoms can also result from excessive mechanical stress or unsuitable machine settings.
How to Investigate
Compare fiber tensile strength and elongation data from the affected material with an approved reference lot.
Review process settings and equipment condition before concluding that the raw material is defective.
Procurement Recommendation
Request available tensile strength and elongation information, including the test method where relevant.
Any acceptance limits should be established according to the mill’s actual requirements.
7. Surface Finish and Static Electricity Problems
Polyester fibers can develop electrostatic charging during processing.
Fiber surface finish, friction, environmental conditions, and equipment configuration can influence static behavior.
Possible Problems
Excessive static may be associated with:
- Fibers adhering to machine surfaces
- Difficulties during opening or carding
- Irregular fiber movement
- Increased fly or fiber accumulation
- Processing instability
Static behavior should be evaluated under the actual production conditions.
How to Investigate
Check the affected fiber lot together with:
- Ambient temperature and relative humidity
- Equipment grounding and maintenance
- Fiber finish compatibility
- Machine speed and operating conditions
- Material handling procedures
Do not assume that increasing humidity alone will resolve every static-related problem.
Procurement Recommendation
Ask whether the fiber has a surface finish appropriate for the intended spinning process.
The supplier should confirm available information about the finish without disclosing unsupported or unverified performance claims.
8. Poor Fiber Opening and Entanglement
Fiber opening prepares compressed staple fiber for downstream processing.
Some materials may be more difficult to open because of their compression condition, finish, crimp, or other characteristics.
Possible Problems
Poor opening may contribute to:
- Fiber clumps
- Uneven feeding
- Irregular carding performance
- Higher waste
- Localized sliver irregularity
- Increased cleaning or maintenance requirements
However, poor opening can also be caused by unsuitable equipment settings or handling practices.
How to Investigate
Compare fiber behavior during opening with a previously approved material.
Inspect the bale condition and check whether the issue persists after equipment settings have been reviewed.
Procurement Recommendation
When introducing a new fiber grade, conduct a controlled production trial before approving large-volume orders.
9. Moisture and Storage-Related Problems
Storage and handling conditions can affect the condition of polyester staple fiber and its packaging.
Although polyester is relatively low in moisture absorption compared with some other textile fibers, storage conditions still matter.
Possible Problems
Poor storage or moisture exposure may contribute to:
- Damaged packaging
- Contamination
- Handling difficulties
- Changes in processing behavior
- Inconsistent bale condition
The severity depends on the actual exposure and material condition.
How to Investigate
Inspect packaging and bale condition when goods arrive.
Review warehouse storage conditions and determine whether the material has been exposed to water, excessive heat, or contamination.
Procurement Recommendation
Agree on packaging requirements, shipment identification, and appropriate storage conditions.
If a shipment appears damaged, document the condition before the material is mixed into normal production.
10. Lot-to-Lot Fiber Quality Variation
A fiber sample may perform satisfactorily during a trial, while a later commercial shipment behaves differently.
This is one reason why lot consistency matters in long-term B2B supply.
Possible Problems
Differences between production lots may affect:
- Carding and drafting stability
- Yarn appearance
- Waste levels
- End-break frequency
- Production settings
- Finished yarn consistency
The variation may involve fiber fineness, length distribution, crimp, finish, contamination, or other characteristics.
How to Investigate
Compare the affected lot with the previously approved lot using the same relevant test methods.
Review production records and operating conditions to identify whether the material, process, or both have changed.
Procurement Recommendation
Establish a clear purchasing specification and agree on the relevant lot identification and inspection requirements.
For recurring orders, retain representative reference samples when practical.
11. Fiber Blending Inconsistency
Blending is common in polyester/cotton, polyester/viscose, and other yarn manufacturing processes.
Inconsistent blending can create yarn defects even when each raw material is individually acceptable.
Possible Problems
Poor blend uniformity may contribute to:
- Uneven yarn appearance
- Variable yarn strength
- Dyeing differences
- Fabric streaks
- Inconsistent downstream performance
How to Investigate
Review the blending ratio, feeding arrangements, material preparation, and process controls.
Check whether the affected fibers are being mixed consistently throughout production.
Procurement Recommendation
When evaluating polyester fiber for blended yarn, provide the supplier with the intended blend composition and spinning system.
Fiber compatibility should be confirmed through actual production trials.
12. How Fiber Quality Issues Affect Yarn Production
The following table summarizes potential relationships between fiber characteristics and spinning symptoms.
| Fiber-Related Issue | Possible Spinning Symptom | Initial Check |
|---|---|---|
| Denier variation | Yarn unevenness | Fiber fineness measurements |
| Cut-length variation | Drafting instability | Staple length distribution |
| Excessive short fibers | Hairiness and waste | Fiber length and process damage |
| Contamination | Visible yarn defects | Bale and opening-line inspection |
| Crimp inconsistency | Carding or drafting variation | Crimp and process settings |
| Tensile variation | Fiber breakage or yarn strength variation | Fiber tensile tests |
| Finish or static problems | Fiber adhesion and handling problems | Finish, humidity and machine conditions |
| Poor fiber opening | Clumps and irregular feeding | Bale condition and opening settings |
| Storage damage | Contamination or handling issues | Packaging and warehouse inspection |
| Lot-to-lot variation | Changing spinning performance | Lot records and comparative testing |
| Blending inconsistency | Uneven composition or appearance | Blend preparation and feeding |
These relationships are diagnostic starting points, not proof of causation.
A spinning mill should verify the actual cause before rejecting a shipment or changing suppliers.
13. How to Distinguish Fiber Problems From Machine Problems
A common mistake in spinning operations is to attribute every yarn defect to the raw material.
A structured investigation can help avoid unnecessary supplier disputes.
Step 1: Identify the Defect
Record the specific symptom, such as yarn unevenness, end breakage, excessive hairiness, or contamination.
Step 2: Check the Distribution
Determine whether the problem occurs across the entire production line, only on selected machines, or only after a particular material change.
Step 3: Compare Material Lots
If possible, compare the affected fiber lot with a previously approved lot under controlled production conditions.
Step 4: Review Machine Settings
Inspect the relevant settings, maintenance condition, feeding arrangements, and environmental controls.
Step 5: Test the Fiber
Use appropriate methods to evaluate the suspected fiber characteristics.
Step 6: Confirm the Root Cause
Document the evidence and identify corrective actions.
A controlled comparison is generally more useful than changing several variables simultaneously.
14. Recommended Fiber Quality Checks for Spinning Mills
Before approving a new recycled polyester staple fiber supplier, buyers may request information on the following parameters.
| Quality Parameter | Why It Matters | Recommended Buyer Action |
|---|---|---|
| Nominal denier | Fiber fineness | Confirm specification and tolerance |
| Cut length | Drafting compatibility | Review length distribution |
| Tensile strength | Mechanical behavior | Request applicable test information |
| Elongation | Response to stress | Compare with approved material |
| Crimp | Fiber cohesion and handling | Confirm relevant characteristics |
| Surface finish | Friction and static behavior | Check process suitability |
| Cleanliness | Contamination control | Agree on inspection criteria |
| Color | Visual consistency | Define required appearance |
| Lot identification | Traceability | Request agreed lot information |
| Packaging | Material protection | Confirm bale and handling requirements |
Not every spinning mill requires the same testing program.
The appropriate inspection plan depends on the spinning system, yarn count, blend composition, customer requirements, and operational risk.
15. Recycled vs Virgin Polyester Fiber: Are Quality Issues Different?
All Recycled and virgin polyester staple fibers belong to the same broad polymer family, but their feedstock origins differ.
Recycled polyester fiber may require particular attention to feedstock consistency and contamination control.
However, recycled polyester is not automatically lower quality than virgin polyester, and virgin fiber is not automatically free from processing problems.
Both materials should be evaluated against the same relevant technical and operational requirements.
For recycled polyester, buyers may additionally request supporting information about recycled content or traceability where required.
Any environmental or certification claim should be verified using applicable documentation.
The most meaningful comparison is how the proposed material performs under the buyer’s actual manufacturing conditions.
16. How to Evaluate a Polyester Staple Fiber Supplier
For international procurement teams, supplier evaluation should cover technical suitability and supply consistency.
Clear Product Specifications
The supplier should identify the offered fiber grade and confirm the relevant characteristics.
Technical Communication
A supplier should be able to discuss denier, cut length, application, and other requirements without assuming that one grade suits every spinning process.
Sample Evaluation
Where practical, request a sample and conduct a controlled spinning trial.
Quality Documentation
Ask which specification sheets, inspection records, and test reports are available for the proposed product.
Lot Consistency
Discuss how production lots are identified and how agreed quality requirements are maintained.
Commercial Reliability
Confirm packaging, order quantity, lead time, Incoterms, and shipment arrangements.
A low initial price may not provide the best purchasing value if processing instability creates additional waste or downtime.
17. Fiber Quality Troubleshooting Checklist for B2B Buyers
Before raising a quality claim with a supplier, collect the following information.
Fiber Identification
- Supplier and product grade
- Nominal denier and cut length
- Production lot or shipment reference
- Received quantity
- Relevant technical specification
Observed Problem
- Description of the defect
- Date and production line
- Affected machines or positions
- Relevant production conditions
- Photographs or retained samples
Technical Investigation
- Incoming fiber inspection
- Comparison with approved material
- Machine setting review
- Environmental condition review
- Applicable fiber tests
- Yarn quality test results
Supplier Communication
- Summary of the observed problem
- Supporting evidence
- Relevant lot information
- Requested technical review
- Agreed corrective-action process
Clear documentation helps both the buyer and supplier investigate the issue efficiently.
18. Sourcing Recycled Polyester Staple Fiber for Yarn Spinning From Vietnam
For international spinning mills, selecting recycled polyester staple fiber requires matching the raw material to the intended yarn and production process.
At Eco Micro Fiber / GDI Textile, we welcome inquiries from manufacturers, importers, and textile procurement teams evaluating recycled polyester staple fiber for suitable spinning applications.
Buyers can share:
- Target yarn count
- Ring, rotor, or vortex spinning system
- Intended fiber blend
- Required denier and cut length
- White or black fiber requirements
- Existing approved fiber specification
- Initial order quantity
- Destination country and port
- Any critical quality or documentation requirements
Our team can review the inquiry and discuss available fiber options, subject to product availability and technical confirmation.
Specific test results, production tolerances, and application suitability should be confirmed before an order is finalized.
Contact GDI Textile
Email: [email protected]
Website: https://ecomicrofiber.com/
Frequently Asked Questions
What are the most common fiber quality issues in polyester yarn spinning?
Common concerns include denier variation, inconsistent cut length, excessive short fibers, contamination, crimp variation, unsuitable surface finish, static behavior, and lot-to-lot inconsistency. Their actual effects depend on the spinning system and process conditions.
Can poor recycled polyester fiber quality cause yarn breakage?
It can contribute to yarn breakage in certain circumstances, but machine settings, drafting conditions, spinning parameters, and other factors can also cause end breaks. A root-cause investigation is necessary.
Why does polyester yarn become uneven?
Yarn unevenness can result from fiber characteristics, blending, drafting, equipment condition, or process variation. Fiber denier and length distribution are among the parameters worth checking.
How does fiber contamination affect yarn quality?
Foreign material may cause visible yarn defects, processing difficulties, additional cleaning, or finished-product rejection. The severity depends on the contaminant and application.
Is recycled polyester staple fiber suitable for fine yarn spinning?
Selected grades may be suitable, depending on fiber fineness, length, spinning system, target yarn count, and quality requirements. Suitability should be verified through technical evaluation and spinning trials.
What should a spinning mill check before approving a new polyester fiber supplier?
The mill should review the product specification, relevant quality parameters, sample performance, process compatibility, lot consistency, and supplier documentation.
Can two polyester fibers with the same denier and cut length behave differently?
Yes. Fibers with the same nominal dimensions may differ in crimp, strength, elongation, finish, cleanliness, and other characteristics that influence processing.
How can buyers reduce quality disputes with polyester fiber suppliers?
Use clear specifications, approved samples where appropriate, agreed test methods, lot identification, and documented procedures for reporting and investigating nonconformities.
Conclusion
Understanding common fiber quality issues in polyester yarn spinning helps manufacturers improve raw material evaluation and investigate production problems more effectively.
Fiber denier, cut length, crimp, tensile properties, cleanliness, finish, and lot consistency all deserve attention.
However, reliable troubleshooting requires examining the entire spinning process rather than assuming that every yarn defect originates from the fiber supplier.
For international B2B buyers, the best approach combines clear purchasing specifications, controlled production trials, appropriate quality testing, and transparent supplier communication.
Looking for recycled polyester staple fiber for your spinning mill?
Contact GDI Textile at [email protected] with your fiber specification, spinning system, target yarn, and purchasing requirements to discuss suitable product options.